Finite capacity planning schedules production within real resource limits, meaning every job is assigned only when the machines, operators, and materials to complete it are actually available. Infinite capacity planning, by contrast, calculates when work should be done based on due dates and standard lead times, without checking whether the required resources are free. The core difference is whether the plan respects physical limits or ignores them. The sections below unpack how each method works, where each fits, and how manufacturers can use them together effectively.
How does finite capacity planning actually work?
Finite capacity planning works by scheduling each production order against a real-time picture of available resources, including machines, operators, tooling, and materials, so that no two jobs are assigned to the same resource at the same time. The system sequences work based on actual availability, shifting tasks forward or backward in time until a feasible slot is found. The result is a schedule that can survive contact with reality.
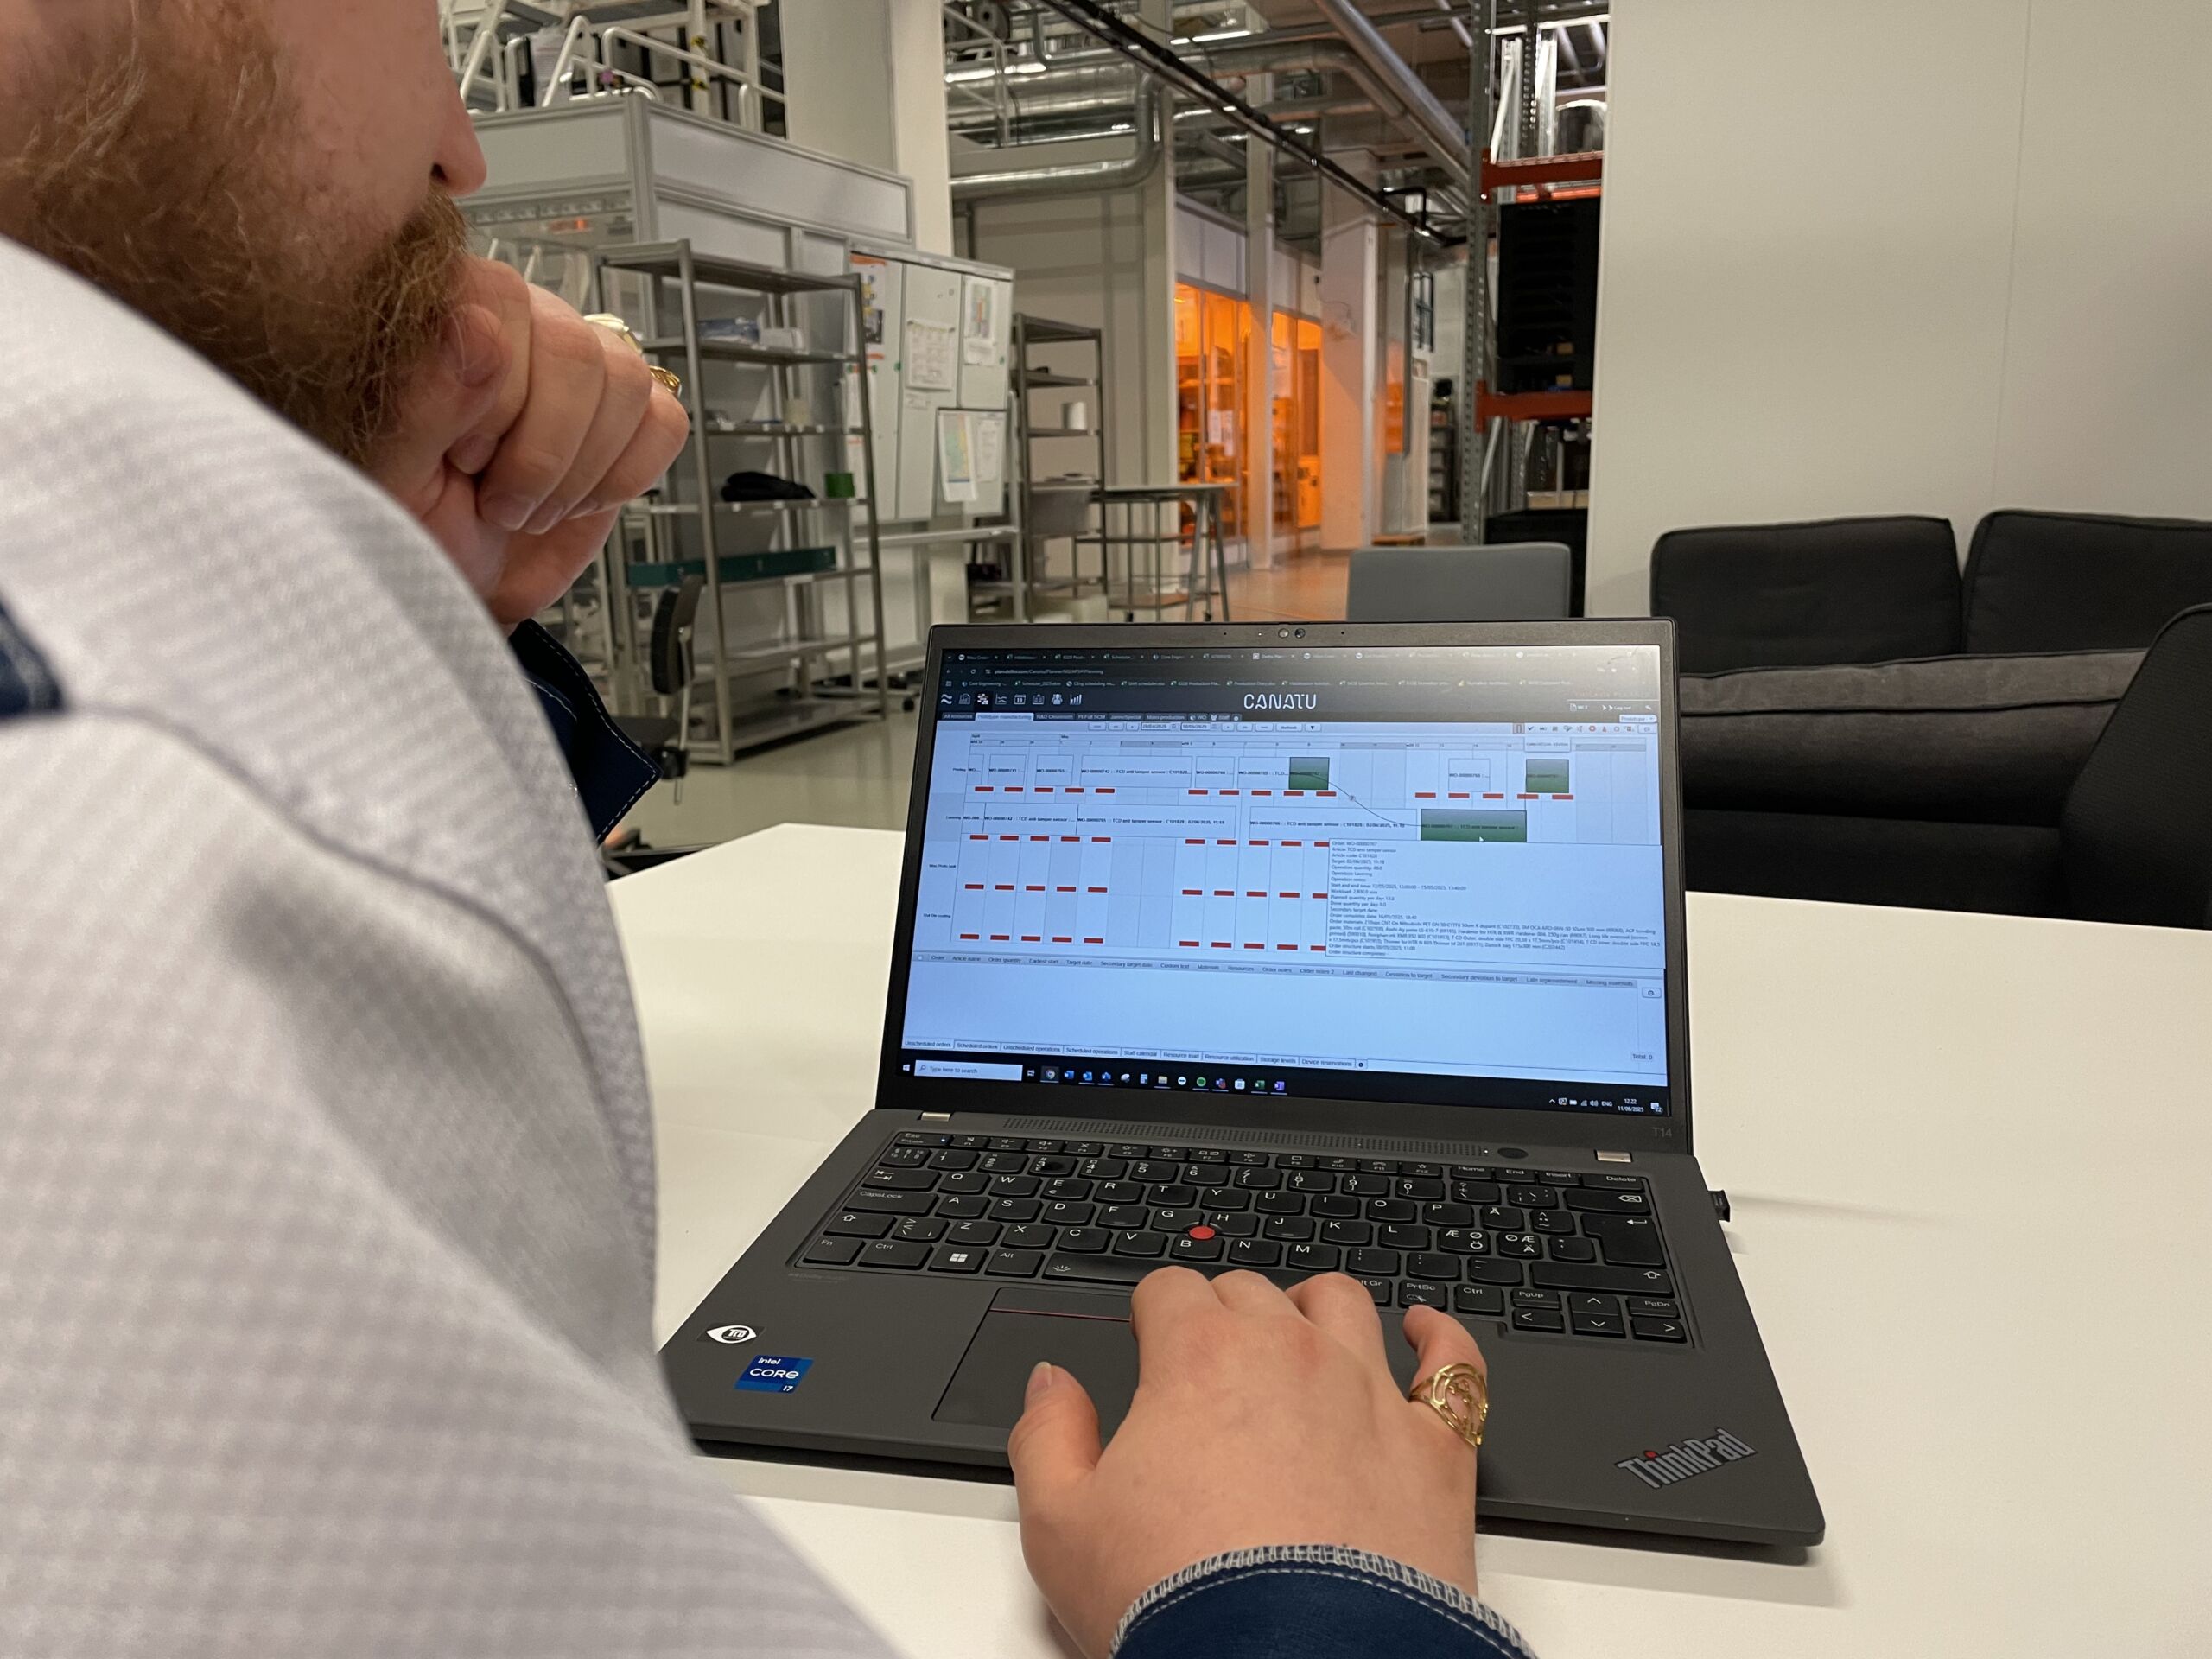
In practice, a finite scheduler holds a live model of the shop floor. When a new order arrives, the system checks every constraint in the chain before committing to a start date. If a machine is already booked, the job waits or is routed to an alternative resource. If a component is delayed, every downstream operation moves accordingly. This constraint-aware logic is what separates finite scheduling from a simple spreadsheet or a standard ERP plan.
Most ERP and MRP systems plan with infinite capacity by default. They backward-schedule from a due date and never verify whether the machine or operator is actually free, so the plan looks clean on paper but collapses the moment a real constraint appears. Layering finite, constraint-based scheduling on top of an ERP fixes this by writing achievable dates back into the system based on what the shop floor can genuinely deliver.
Underpinning all of this is routing data. A routing defines the sequence of production operations required to complete a product, specifying which work center performs each step, how long each step takes (including setup time and run time), and the order in which those steps must occur. Without accurate routing data, a finite scheduler cannot determine which resources are needed, for how long, or in what operation sequence, making constraint checking impossible. Maintaining up-to-date routings is therefore a practical prerequisite for any finite scheduling implementation, and the quality of the schedule output is directly tied to the accuracy of this underlying data.
What is infinite capacity planning used for?
Infinite capacity planning is used for high-level demand planning, sales forecasting, and rough-cut capacity analysis, where the goal is to understand whether a production volume is broadly achievable over a longer horizon rather than to produce an executable daily schedule. It answers questions like “Can we take on this order?” before committing to a customer, without the computational overhead of a full constraint check.
Infinite planning is a useful starting point in the planning hierarchy. When a business needs to model several demand scenarios quickly, or when a sales team needs a fast lead-time estimate, infinite capacity gives a directional answer quickly. It is also commonly used in master production scheduling at a weekly or monthly level, where small daily imbalances are assumed to average out over time.
The important caveat is that infinite capacity planning is a planning tool, not a scheduling tool. The moment a plan needs to translate into actual shop-floor instructions, resource constraints must enter the picture. Using infinite planning alone to drive execution is where manufacturers run into missed due dates and overloaded work centers.
What are the key differences between finite and infinite capacity planning?
The key difference between finite and infinite capacity planning is that finite planning enforces resource constraints when building the schedule, while infinite planning ignores them. Finite planning produces an executable sequence of work orders; infinite planning produces a theoretical load picture that still needs to be validated against real capacity before it can be acted on.
The differences play out across several practical dimensions:
- Resource visibility: Finite planning requires a detailed model of machines, people, and materials. Infinite planning works with aggregate capacity figures or none at all.
- Schedule accuracy: Finite schedules are achievable by design. Infinite schedules are optimistic by design and require manual adjustment.
- Planning horizon: Infinite planning suits week-to-month horizons. Finite planning is most valuable at the day-to-week execution level.
- Computational complexity: Finite scheduling is more demanding to set up and run, because it must solve a real constraint-satisfaction problem. Infinite planning is faster and simpler.
- Response to disruption: A finite scheduler can resequence automatically when a machine breaks down or a job is expedited. An infinite plan has no mechanism to absorb disruption.
How do ERP systems handle finite and infinite capacity planning?
Most ERP systems, including SAP, default to infinite capacity planning in their standard planning runs. Tools like CM50 (Capacity Evaluation) allow planners to view load versus available capacity per work center across a defined time horizon, giving a useful overview of where demand exceeds supply. This capacity evaluation view helps planners spot potential overloads before they become a problem on the shop floor, but it does not resolve those overloads automatically.
SAP’s CM21 (Capacity Leveling) takes this a step further by providing a graphical planning table where planners can manually shift operations between time periods to smooth out overloads. This capacity leveling functionality gives planners direct control over the schedule, but it remains a largely manual process. When you are dealing with dozens of work orders competing for the same resources across multiple work centers, manually dragging and dropping operations quickly becomes unmanageable, especially when priorities change overnight.
This is where dedicated Advanced Planning and Scheduling (APS) solutions add real value. Rather than replacing the ERP, an APS layer sits on top of it and applies automated, constraint-based finite scheduling to the demand signal coming from the ERP. Instead of a planner spending hours leveling capacity manually, the scheduler resolves conflicts algorithmically and produces a sequenced, executable plan in minutes. For manufacturers who have already invested in SAP or another ERP, this kind of APS integration is often the most practical path to genuinely finite scheduling.
When should a manufacturer choose finite over infinite scheduling?
A manufacturer should choose finite capacity scheduling when production runs close to capacity, when due-date reliability is commercially critical, or when the shop floor has bottleneck resources that regularly constrain output. In these conditions, an infinite plan will consistently overcommit the business and erode customer trust.
Finite scheduling becomes especially important in environments with high product mix, short lead times, or frequent order changes. When dozens of different jobs compete for the same machine in the same week, only a constraint-aware scheduler can produce a sequence that actually works. Trying to manage this with an infinite plan means a planner spends most of their day manually firefighting the gap between what the system promised and what the floor can deliver.
High-volume, repetitive manufacturing with stable, predictable demand and ample spare capacity is the scenario where infinite planning can hold up on its own for longer. But as variability increases and margins tighten, the case for finite scheduling for production planning strengthens considerably.
What are the limitations of infinite capacity planning?
The main limitation of infinite capacity planning is that it produces schedules that cannot be executed as-is. Because the method does not account for resource availability, it routinely overloads work centers, generates unrealistic lead times, and creates due-date commitments the shop floor cannot meet. The plan looks complete, but it is not actionable without significant manual intervention.
Other practical limitations include:
- Hidden bottlenecks: Infinite planning cannot identify which resources are genuinely constraining throughput, because it never models resource utilization at a granular level.
- Poor change response: When a machine breaks down or a priority order arrives, an infinite plan offers no automatic way to resequence. Every change requires a planner to rebuild the schedule manually.
- False confidence: A neatly printed infinite schedule can create the impression that production is under control when it is not, delaying the recognition of a capacity problem until it becomes a crisis.
- Cumulative error: In complex multi-stage production, small inaccuracies at each stage compound into large delivery errors by the time a job reaches final assembly.
These limitations do not make infinite planning worthless. They do mean that any manufacturer using infinite planning for execution-level scheduling is accepting a structural gap between plan and reality.
Can finite and infinite capacity planning be used together?
Yes, finite and infinite capacity planning are most effective when used together at different levels of the planning hierarchy. Infinite planning handles the longer-horizon demand and sales picture, while finite scheduling takes over at the execution level to turn that demand signal into an achievable, sequenced production plan.
This layered approach is how modern production planning environments typically operate. An MRP or ERP system runs infinite planning to generate a rough production requirement across weeks or months. A finite scheduling layer then takes that requirement and resolves it against real shop-floor constraints, producing a daily or weekly schedule that planners and operators can actually follow.
The handoff between the two layers is where most planning problems occur. If the finite scheduler is not tightly integrated with the demand signal coming from the infinite plan, the two systems drift apart and planners are left reconciling conflicting information. The goal is a seamless flow from demand forecast through to sequenced shop-floor instructions, with each layer doing the job it is genuinely suited for. Getting that integration right is, in our experience, one of the highest-value improvements a manufacturing business can make to its planning process.
How does finite capacity planning work with forecasting?
Finite capacity planning with forecasting addresses a challenge that every production planner knows well: confirmed orders rarely cover the full planning horizon, yet capacity decisions cannot wait until the order book is full. In industries with long lead times, seasonal demand peaks, or extended supplier lead times, waiting for firm orders before loading capacity means you will always be reacting too late. A finite scheduler can consume a forecast signal, whether it comes from an S&OP process, an MRP run, or a sales projection, and allocate capacity against it while still enforcing real resource constraints. The result is a forward-looking schedule that is grounded in what the shop floor can actually deliver, not just what demand theory suggests.
In practice, this means the finite scheduler treats forecast demand much like confirmed orders, assigning it to specific work centers and time slots based on routing data, available capacity, and sequencing rules. If a work center is already loaded with firm orders, forecast-driven jobs are pushed to the next available slot rather than stacked on top of existing commitments. This gives planners a realistic view of how much headroom remains for new orders and where capacity investments or overtime decisions may be needed weeks in advance, rather than days after a problem has already emerged.
When actual orders arrive and differ from the forecast, a finite scheduler can resequence against the updated demand without requiring a manual rebuild of the entire schedule. If a confirmed order is larger than the forecast suggested, the system identifies the impact on downstream operations and flags the constraint. If demand comes in lower, capacity is freed up and can be reallocated. This ability to absorb forecast-to-actuals variation automatically is one of the most practical advantages of finite capacity planning with forecasting, and it is a significant step up from managing the same situation with spreadsheets or a standard ERP plan alone.
Frequently asked questions about finite and infinite capacity planning
What is finite capacity planning?
Finite capacity planning is a scheduling method that assigns production orders only to time slots where the required resources, including machines, operators, and materials, are confirmed as available. It produces a schedule that reflects what the shop floor can genuinely deliver, rather than what would be theoretically possible if resources were unlimited. This makes it the foundation of reliable due-date commitments and realistic shop-floor instructions.
What is infinite capacity planning?
Infinite capacity planning calculates when production work should occur based on due dates and standard lead times, without checking whether the necessary resources are actually free at that time. This makes it useful for high-level demand planning and rough-cut capacity analysis, but it is not suited for executable shop-floor scheduling. The schedules it produces require manual validation and adjustment before they can be acted on.
What does finite capacity mean in manufacturing?
In manufacturing, finite capacity means that the planning system treats every resource as having a fixed, limited number of available hours per period and will not schedule more work than those hours allow. Rather than assuming a machine or work center can absorb any amount of demand, the system enforces real boundaries and sequences work accordingly. This is what separates a plan that looks good on paper from one that the shop floor can actually execute.
Why does finite capacity scheduling matter for manufacturers?
Finite capacity scheduling matters because it eliminates the gap between what the plan promises and what the shop floor can actually deliver. By enforcing real resource constraints during scheduling, it reduces missed due dates, prevents work center overloads, and gives planners a reliable basis for customer commitments. For production planners specifically, it replaces the constant cycle of manual firefighting with a schedule that holds up when conditions change, freeing up time for genuine planning rather than reactive problem-solving.